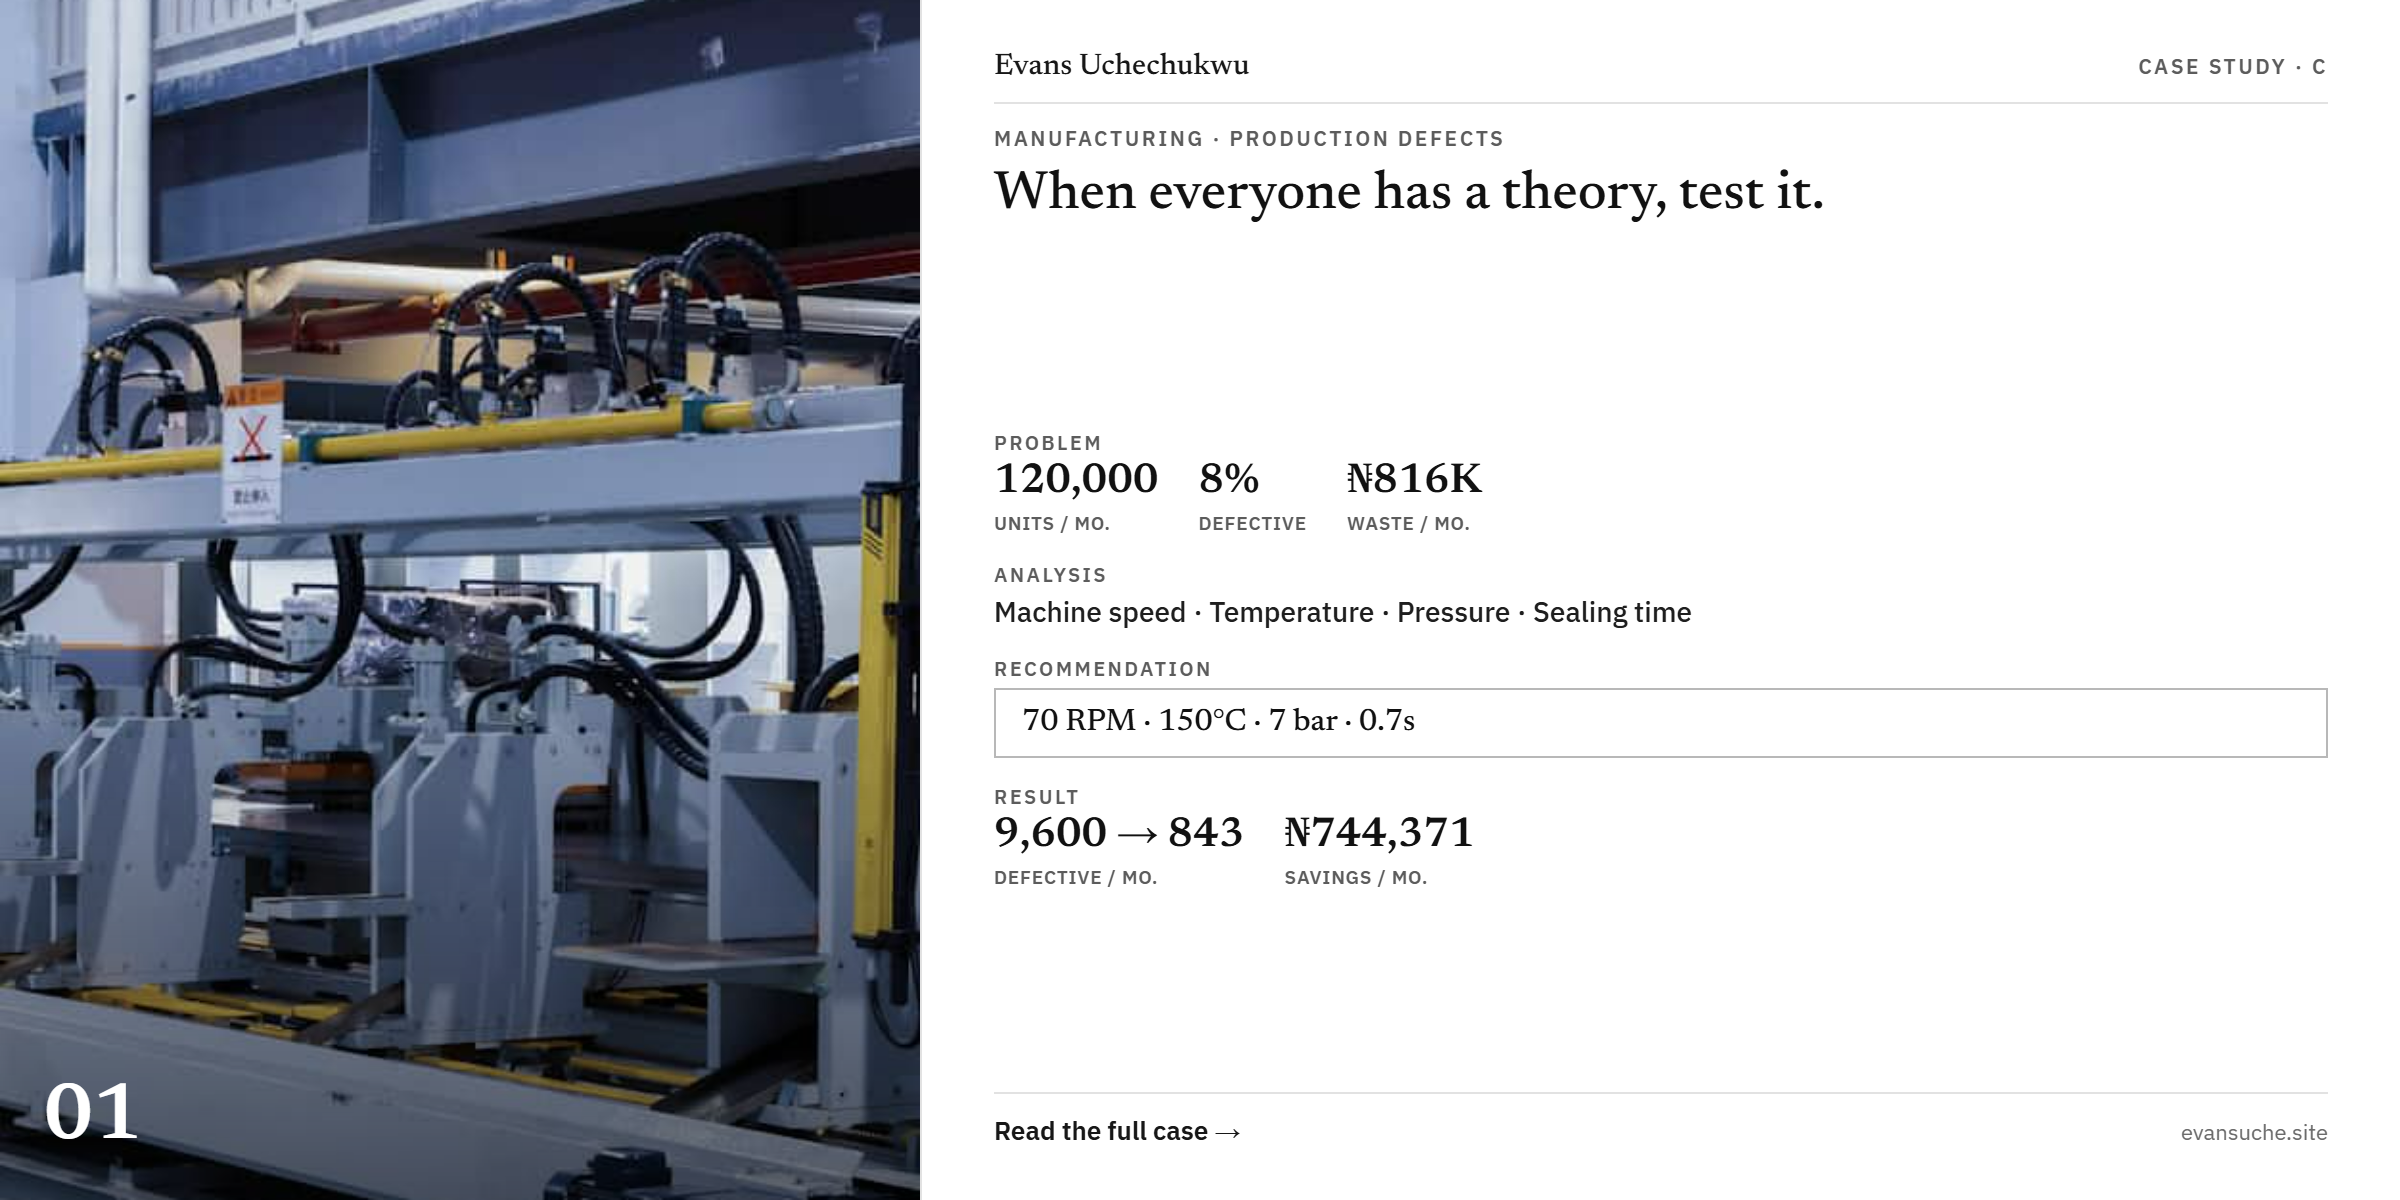
A manufacturer produces about 120,000 units every month.
Recently, something has gone wrong.
The percentage of defective products has risen to around 8%.
At that rate, approximately 9,600 units are being rejected every month.
At an estimated cost of ₦85 per defective unit, that represents roughly ₦816,000 in direct monthly waste before considering rework, delays, customer complaints and other consequences.
Management has theories about the cause.
The production manager thinks the machine is running too fast.
The technician suspects temperature.
The operator thinks pressure is the problem.
Someone else believes the raw material is responsible.
The problem is not that they lack ideas.
The problem is that nobody knows which explanation is actually correct.
So rather than changing one setting, observing what happens, and then changing another, I approached the problem differently.
We designed an experiment.
The problem
The production process had four controllable settings:
| Factor | Low Setting | High Setting |
|---|---|---|
| Machine speed | 55 RPM | 70 RPM |
| Temperature | 150°C | 170°C |
| Pressure | 5 bar | 7 bar |
| Sealing Time | 0.4 seconds | 0.7 seconds |
Each of these could potentially affect the defect rate.
But there was an important complication.
The factors might not act independently.
For example, perhaps increasing machine speed does little when the temperature is low, but causes serious problems when the temperature is high.
If that were true, looking at speed by itself could lead to the wrong conclusion.
The question therefore wasn't simply:
“Which factor causes defects?”
It was:
“Which factors matter, and do particular combinations of settings create problems?”
We tested the combinations
With four factors, each at two levels, there are:
2⁴ = 16 possible combinations.
Each combination was replicated three times, producing 48 experimental runs.
For each run, the production process was operated at the specified settings and the number of products produced and rejected was recorded.
The resulting dataset contained 48 observations, with 250 units produced in each run.
This matters because we aren't simply comparing two percentages and hoping the difference means something.
Replication allows us to observe the natural variation in the process.
The experiment gives us a way to separate that ordinary variation from effects that are large enough to matter.
The result was not what management would expect
The analysis tested the individual factors as well as their interactions.
The strongest individual effects were temperature and pressure.
But the most interesting result was the interaction between:
machine speed × temperature.
Machine speed by itself was not statistically significant.
The interaction between speed and temperature, however, was extremely strong.
In other words:
Speed wasn't simply “bad.”
Temperature wasn't simply “bad.”
The combination of the two was the problem.
This is an important distinction.
A manager looking only at averages might conclude:
“The machine speed isn't the problem.”
And technically, that conclusion could be correct.
But it would miss the much more important finding:
High speed becomes a problem under the wrong temperature condition.
The analysis found the speed × temperature interaction to be the dominant effect in the experiment, while speed alone did not reach the 5% significance threshold.
Finding the better operating conditions
The analysis identified the following combination as the recommended operating point:
70 RPM
150°C
7 bar
0.7 seconds
At this setting, the observed defect rate in the experimental data was as low as 0.53%, while the reduced statistical model estimated an expected defect rate of approximately 0.70%.
That is dramatically different from the original 8% defect rate.
If the manufacturer maintained approximately 120,000 units of monthly production, the estimated reduction would be from around:
9,600 defective units → 843 defective units per month.
At ₦85 of direct cost per defective unit, that represents approximately:
₦744,371 in projected monthly savings.
But there was still one more thing to do.
We tested the recommendation
A statistical recommendation shouldn't simply be accepted because the numbers look good.
The recommended settings were tested again using a fresh confirmation run.
This time, 15 out of 1,500 units were rejected, giving an observed defect rate of:
1.00%
The predicted rate from the analysis was 0.70%.
The confirmation result was statistically consistent with that prediction; the report gives a p-value of 0.1623 and a 95% confidence interval of approximately 0.56%–1.64% for the observed rate.
The important point isn't that the prediction was exactly 0.70% and the confirmation was exactly 0.70%.
Real processes don't behave that neatly.
The important point is that a new set of observations supported the conclusion reached from the original experiment.
What was actually learned?
The obvious conclusion is:
The manufacturer can potentially reduce its defect rate dramatically.
But there is a more interesting conclusion.
Everyone involved had a theory.
And almost everyone had part of the truth.
The machine speed mattered in combination with temperature.
Temperature mattered.
Pressure mattered.
But none of the simple explanations captured the whole problem.
The problem was in the interaction between operating conditions.
That is one of the reasons structured experimentation can be so valuable.
Businesses often change one thing, observe the result, change another thing, and try to remember what happened.
Sometimes that works.
But when several variables influence an outcome simultaneously, intuition can struggle to separate their effects.
A properly designed experiment can.
What this means for a business
This approach isn't limited to defective products.
The same principle can apply whenever a business has:
a measurable outcome,
several factors that may influence it,
and enough control over those factors to test them deliberately.
For example:
Manufacturing
Which machine settings minimise waste?
Food production
Which combination of temperature, cooking time and ingredients produces the best quality?
Marketing
Which combination of offer, timing and messaging produces the most profitable response?
Operations
Which process configuration reduces turnaround time?
Customer experience
Which intervention actually increases repeat purchases?
The question is not always:
“What does the data say?”
Sometimes the better question is:
“What experiment should we run so that the data can answer the question?”
What a business needs before this kind of analysis
A business doesn't need to arrive with a perfectly formatted statistical dataset.
It needs a business problem.
For example:
“Our defect rate has increased and we don't know why.”
From there, the analysis begins with understanding the process.
What outcome are we trying to improve?
What factors could plausibly influence it?
Which of those factors can actually be changed?
What ranges are safe and commercially realistic?
How many experimental runs can the business reasonably perform?
What should remain controlled?
Once those questions are answered, an appropriate experimental design can be created.
The business then performs the runs and records what actually happened.
The statistics come after the experiment.
That distinction is important.
The analysis cannot manufacture real-world evidence.
It can only extract information from observations that actually occurred.
The bigger idea
A business can spend months arguing about why something is going wrong.
The production manager can have one theory.
The technician can have another.
The operator can have a third.
And they can all sound reasonable.
But sometimes the most useful thing you can do is stop arguing about the theories and design a way to test them.
In this case, the analysis revealed something that wasn't obvious from the individual factors alone:
The problem wasn't simply machine speed or temperature. It was what happened when the two were combined.
That is the value of statistical analysis; finding something about the business that wasn't obvious before, and turning that finding into a better decision.
Case result
Original defect rate: 8.00%
Predicted defect rate: 0.70%
Confirmation run: 1.00%
Projected monthly defects: 9,600 → 843
Projected monthly savings: ₦744,371/month
Key finding: Speed × temperature interaction was the dominant effect.